
Precision metal stamping parts are among the most cost-effective ways to produce high-volume metal components — but only when the stamping process is correctly matched to the part's geometry, material, tolerance, and production volume requirements. Getting precision metal stamping parts right means making the right decisions at the design stage: choosing the correct material grade and temper, designing the geometry for stamping manufacturability, specifying tolerances that the stamping process can consistently hold, and planning for the tooling investment that the production volume justifies. This precision metal stamping parts buyer's guide walks through the process from design through production, explaining what drives cost and quality in precision metal stamping parts sourcing and how to select a stamping supplier whose capabilities match the application.
Understanding the Precision Metal Stamping Process
Metal stamping uses a die — an engineered tool with male and female cavities — to form sheet or strip material into three-dimensional shapes through compressive force applied by a press. In precision metal stamping parts production, the press delivers controlled force through a guided ram, the die controls the material's deformation path, and the stripper, blank holder, and pilot pin systems control material flow and part position during each press stroke. The key characteristic of precision metal stamping parts is repeatability: once the die is qualified and the process parameters are established, each stroke produces a part identical to the last within the tolerances the die was designed to hold. This repeatability is what makes precision metal stamping parts the lowest-cost method for producing high-volume metal components — and the reason that tooling investment is justified only at sufficient production volumes.
The precision metal stamping parts process types include:
Progressive die stamping — the strip advances through multiple die stations with each press stroke, with each station performing a different operation (blank, draw, pierce, form, trim) until the completed part exits the die at the final station. Used for complex precision metal stamping parts requiring multiple operations.
Transfer die stamping — the blank is moved mechanically between stations rather than carried on the strip. Used for very large precision metal stamping parts where the part must be separated from the strip before subsequent operations.
Compound die stamping — multiple operations (blank and pierce, blank and draw) are performed in a single press stroke at a single die station. Used for simpler precision metal stamping parts where the part geometry is achievable in one or two operations.
Four-slide/multislide stamping — four or more tooling heads form the part from the sides simultaneously, producing complex cross-sectional geometries that progressive dies cannot achieve. Used for precision metal stamping parts like clips, terminals, and contacts.
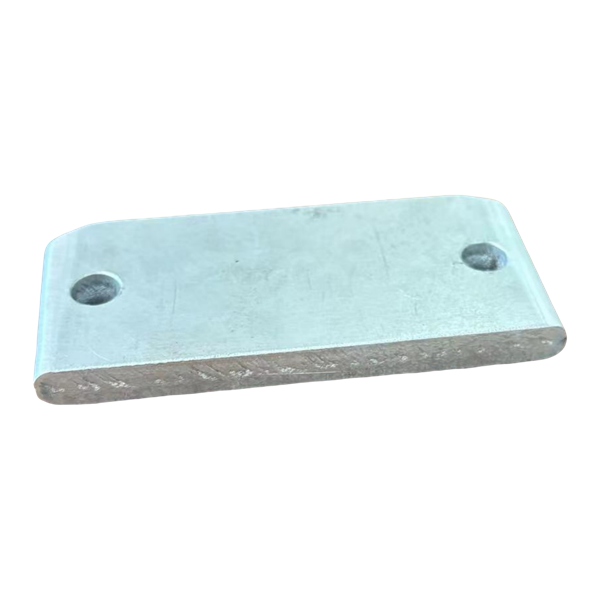
Why Precision Matters in Precision Metal Stamping Parts
Precision in precision metal stamping parts is not just about dimensional tolerance — it is about the relationship between stamping process capability and the assembly requirements that the stamped parts must satisfy. A precision metal stamping parts tolerance of ±0.005 inches means nothing if the part must mate with other components and the cumulative tolerance stack from multiple stamped parts, fasteners, and weld joints exceeds the assembly clearance. Understanding precision metal stamping parts capability means evaluating the process against the full assembly requirement, not just the individual part dimension.
Material Selection for Precision Metal Stamping Parts
The material for precision metal stamping parts is selected based on the combination of mechanical properties required (strength, hardness, ductility), corrosion resistance, formability, and cost. The most commonly stamped materials are:
Low carbon steel (SPCC, DC01, AISI 1008/1010) — the most economical precision metal stamping parts material, with good formability in low-carbon grades and reasonable strength in higher-carbon grades (AISI 1018/1020). Used for brackets, clips, structural components.
Stainless steel (301, 304, 430) — specified for precision metal stamping parts requiring corrosion resistance, typically in the annealed or 1/4 hard temper for stamping formability. 301 stainless work-hardens rapidly during forming, requiring higher force and specific die clearance.
Aluminum (5052, 3003) — specified for precision metal stamping parts where weight reduction or corrosion resistance is important. Aluminum has approximately one-third the density of steel, enabling lighter precision metal stamping parts without sacrificing stiffness if section geometry is appropriately designed.
Copper alloys (brass C260, phosphor bronze C510) — specified for precision metal stamping parts requiring electrical conductivity, corrosion resistance, or spring properties. Copper alloys are more expensive and require specific die materials due to their tendency to gall against steel tooling.
Material Temper and Its Effect on Precision Metal Stamping Parts
The temper designation on precision metal stamping parts materials — H32, H34, T6, O — determines the balance between strength and formability. Annealed (O) temper material is most formable — suitable for deep drawing and complex forming. H-temper (work-hardened) materials have higher strength but reduced formability — suitable for precision metal stamping parts that require moderate forming with higher finished-part strength. T-temper (solution heat-treated and aged) materials like 6061-T6 aluminum have the highest strength but the lowest formability — requiring warm forming or specialized die designs for precision metal stamping parts with complex geometry.
Tolerances Achievable in Precision Metal Stamping Parts
The tolerances achievable in precision metal stamping parts depend on the specific dimension, the stamping operation type, the material, and the supplier's process control capability. General tolerances for precision metal stamping parts are:
Pierced holes: ±0.003 to ±0.005 inches for hole diameter in the 0.030 to 0.500 inch range, with positional accuracy of ±0.003 to ±0.008 inches depending on pilot pin guidance and strip advancement accuracy.
Bent flanges: angular tolerance of ±0.5 to ±1.0 degrees on bend angle; positional tolerance of ±0.010 to ±0.020 inches on bend location.
Drawn shells: wall thickness tolerance of ±10 to ±15 percent of nominal; diameter tolerance of ±0.005 to ±0.015 inches on drawn diameters.
Overall part dimensions: ±0.005 to ±0.020 inches on major dimensions depending on part size, material thickness, and die design.
Tighter tolerances in precision metal stamping parts — below the standard ranges above — require secondary machining operations (CNC machining, grinding) that add cost and cycle time. Designing precision metal stamping parts with tolerances appropriate to the stamping process reduces cost and improves producibility compared to specifying tight tolerances that require secondary machining on every part.
Cpk Requirements for Precision Metal Stamping Parts
The process capability index (Cpk) for precision metal stamping parts production describes how consistently the stamping process produces parts within the specified tolerance. Cpk ≥ 1.33 indicates a capable process — one that produces parts within tolerance with adequate safety margin. Cpk ≥ 1.67 indicates a highly capable process suitable for precision metal stamping parts with critical safety or fit characteristics. A stamping supplier that can provide Cpk data from comparable precision metal stamping parts production demonstrates the process control that repeatable quality requires.
Tooling Considerations for Precision Metal Stamping Parts
The die is the heart of precision metal stamping parts production — and tooling investment is the most consequential cost decision in stamping sourcing. Progressive dies for complex precision metal stamping parts can cost $30,000 to $200,000 depending on complexity, number of stations, and die material (tool steel for standard production volumes, carbide inserts for high-volume runs). The tooling investment is justified when the production volume is sufficient to amortize the tooling cost over the part price — a calculation that must be done before committing to the precision metal stamping parts sourcing decision.
For precision metal stamping parts with moderate volumes (5,000 to 50,000 pieces), compound dies or simple progressive dies with fewer stations provide the best cost-to-tolerance balance. For very low volumes (below 5,000 pieces), stamped parts from simple progressive dies or single-action dies are typically more economical than custom tooling investment. For precision metal stamping parts at prototype stage, short-run tooling with softer tool steel or 3D-printed tooling provides a lower-cost option for design validation before committing to production tooling.
Tooling Ownership and Maintenance in Precision Metal Stamping Parts
The ownership and maintenance terms for stamping tooling in precision metal stamping parts sourcing should be negotiated before tooling is commissioned. Standard practice is that the customer owns the tooling — paying for the initial tooling investment — and the supplier maintains it under a tooling maintenance agreement. The maintenance agreement should specify the maintenance schedule, the wear items covered, the response time for emergency die repairs, and the tooling storage conditions. A stamping supplier that stores precision metal stamping parts tooling in climate-controlled facilities with documented maintenance records provides better tooling protection than one that stores dies in uncontrolled warehouse conditions.
Secondary Operations in Precision Metal Stamping Parts
Most precision metal stamping parts require secondary operations beyond the stamping press: deburring, tumbling, and vibratory finishing to remove sharp edges and improve surface finish; heat treatment to achieve target hardness and strength; plating, anodizing, or powder coating for corrosion resistance and appearance; welding or clinching to join stamped parts into assemblies; and CNC machining for features that the stamping die cannot produce to the required tolerance. An integrated precision metal stamping parts supplier with in-house secondary operations provides better coordination and faster problem resolution than one that outsources secondary work to separate vendors.
Supplier Qualification for Precision Metal Stamping Parts
Qualifying a precision metal stamping parts supplier follows the same structured process as qualifying any precision manufacturing supplier: quality system verification (ISO 9001 or sector-specific), equipment capability assessment, first article inspection, and production performance monitoring. The specific areas to evaluate in a precision metal stamping parts supplier audit include: die design and build capability (in-house or outsourced die building affects lead time and engineering change responsiveness); press capacity (tonnage and bed size relative to the part size and material thickness); material sourcing (from approved mills with traceability); and Cpk data from comparable precision metal stamping parts production runs.
Conclusion
Sourcing precision metal stamping parts effectively requires matching the stamping process to the part's geometry, material, tolerance, and volume requirements from the design stage — not trying to force a stamping solution onto a part designed without manufacturability in mind. The precision metal stamping parts buyer's key decisions — material grade and temper, tolerance specification, tooling strategy, and supplier qualification — all interact. A stamped part designed for stamping manufacturability, with tolerances appropriate to the process, with tooling investment justified by the production volume, and sourced from a qualified stamping supplier with documented process capability, delivers the lowest total cost per part over the production life. When sourcing precision metal stamping parts, invest in the design review phase to ensure the part geometry supports stamping — the cost savings in tooling, per-part price, and production consistency will compound across the production life of the product.
FAQ
What tolerances can precision metal stamping parts achieve?
Precision metal stamping parts achieve hole diameter tolerances of ±0.003 to ±0.005 inches, positional accuracy of ±0.003 to ±0.008 inches, and bend angle tolerances of ±0.5 to ±1.0 degrees. Tighter tolerances require secondary machining.
What materials are used in precision metal stamping parts?
Common precision metal stamping parts materials include low carbon steel (SPCC, DC01), stainless steel (301, 304, 430), aluminum (5052, 3003), and copper alloys (brass C260, phosphor bronze C510).
What is the minimum production volume for precision metal stamping parts?
For precision metal stamping parts with custom tooling, minimum production volumes of 5,000 to 10,000 pieces typically justify the tooling investment. Lower volumes may use simpler dies or standard catalog dies.
What secondary operations do precision metal stamping parts require?
Common secondary operations for precision metal stamping parts include deburring, heat treatment, surface finishing (plating, anodizing, powder coating), welding or clinching for assembly, and CNC machining for features beyond stamping capability.
References
1. ASM Handbook Volume 14B: "Metalworking: Sheet Forming," ASM International, Materials Park, 2005.
2. Hosford, W.F. and Caddell, R.M., "Metal Forming: Mechanics and Metallurgy," 4th Edition, Cambridge University Press, Cambridge, 2011.
3. Davies, R. and Hopper, D., "Stamping Tooling: Diagnosing and Solving Stamping Problems," 2nd Edition, Society of Manufacturing Engineers, Dearborn, 2005.
4. Kalpakjian, S. and Schmid, S.R., "Manufacturing Engineering and Technology," 7th Edition, Pearson, Upper Saddle River, 2017.
5. Montgomery, D.C., "Introduction to Statistical Quality Control," 7th Edition, Wiley, Hoboken, 2012.