
Laser cutting sheet metal services have largely replaced plasma cutting, waterjet, and mechanical shearing in high-precision fabrication shops—not because laser is always the cheapest method, but because laser cutting sheet metal services deliver the combination of accuracy, edge quality, and speed that most industrial buyers actually need. If you've been evaluating laser cutting sheet metal services for your parts and wondering whether the accuracy claims are real and how to verify them, this article breaks down what laser cutting sheet metal services actually deliver versus what marketing materials promise.
How Laser Cutting Sheet Metal Services Actually Work
Laser cutting sheet metal services use a focused high-power laser beam—typically 1 to 15 kilowatts on industrial fiber or CO2 machines—to melt, burn, or vaporize material along a programmed path. The laser beam is directed by CNC motion control systems that position the cutting head with positional accuracy of ±0.003 to ±0.005 inches on modern laser cutting sheet metal services equipment. Assist gas—nitrogen for oxide-free cuts on stainless and aluminum, oxygen for faster cuts on carbon steel, compressed air for economical cuts on thinner materials—is coaxial with the laser beam and blows the molten material from the kerf as the cut progresses. The result is a narrow kerf—typically 0.006 to 0.020 inches wide depending on material thickness and laser power—that produces minimal heat-affected zone and a clean edge that often requires no secondary machining.
Fiber Laser Versus CO2 Laser Cutting Sheet Metal Services
Modern laser cutting sheet metal services predominantly use fiber laser technology, which delivers the beam through fiber optic cable rather than mirrors. Fiber lasers are approximately 30 percent more energy-efficient than equivalent-power CO2 lasers, require less maintenance (no mirror alignment), and produce a shorter wavelength that is absorbed more efficiently by metals—particularly copper, brass, and aluminum. Laser cutting sheet metal services using fiber lasers achieve higher cutting speeds on thin materials (0.060 to 0.187 inch) and better edge quality on reflective alloys than CO2-based services. CO2 laser cutting sheet metal services retain an advantage on thicker materials above 0.500 inch in stainless and above 0.375 inch in aluminum, where the longer wavelength produces a cleaner cut edge despite the lower energy efficiency.
Accuracy Capabilities of Laser Cutting Sheet Metal Services
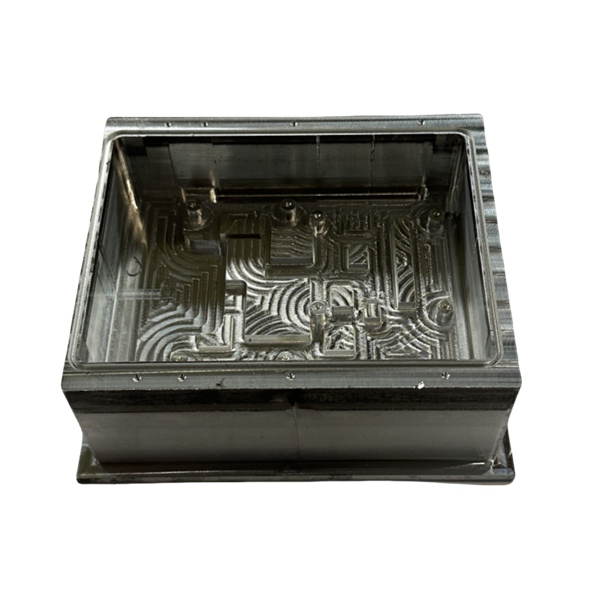
The positional accuracy specification of a laser cutting sheet metal services machine—the machine's ability to position the cutting head at a programmed coordinate—is the upper limit of what laser cutting sheet metal services can deliver. Modern laser cutting sheet metal services equipment with linear encoders and ball screw drives achieves positional accuracy of ±0.003 inches and repeatability of ±0.001 inches on a positioning envelope of 60 by 120 inches or larger. This accuracy supports laser cutting sheet metal services production of parts where feature-to-feature dimensions must be held to ±0.005 inches—a level of precision that matches or exceeds what many CNC machining operations achieve on similar geometries.
What Affects Actual Accuracy in Laser Cutting Sheet Metal Services
The specified machine accuracy is the theoretical performance of laser cutting sheet metal services under ideal conditions. Actual cutting accuracy is degraded by several factors that laser cutting sheet metal services providers manage with varying effectiveness. Thermal expansion of the sheet during cutting causes the part geometry to drift slightly as heat accumulates, particularly on longer cutting sequences with minimal lead-in transitions. Nozzle wear changes the assist gas stream diameter and position, degrading cut edge quality and increasing kerf width over time. Sheet thickness variation—the commercial tolerance on sheet material is typically ±0.005 to ±0.010 inches—changes the energy density per unit thickness, affecting the kerf width and heat input into the part. A well-run laser cutting sheet metal services operation manages these factors through cutting parameter optimization for each material and thickness, nozzle replacement schedules, and cutting sequence planning that minimizes heat accumulation.
Edge Quality from Laser Cutting Sheet Metal Services
Edge quality is one of the strongest advantages of laser cutting sheet metal services over mechanical cutting methods. A laser-cut edge on carbon steel below 0.250 inch is typically square within 1 to 2 degrees of perpendicular, with a surface finish of Ra 64 to Ra 250 µin depending on material thickness and cutting speed. For laser cutting sheet metal services on stainless steel, the nitrogen assist gas produces a bright, oxide-free cut edge suitable for cosmetic or welding applications without secondary machining. For laser cutting sheet metal services producing parts for welding, the narrow kerf and minimal heat-affected zone mean that the cut edge requires minimal prep—often just a light grind to remove the dross from the bottom of the cut.
Dross and Kerf Quality in Laser Cutting Sheet Metal Services
Dross—molten material that re-solidifies on the bottom of the cut—is the primary edge quality defect in laser cutting sheet metal services and it is directly related to the quality of the assist gas delivery system and the cutting parameters selected for the material thickness. Dross-free cutting on carbon steel with laser cutting sheet metal services requires oxygen assist gas pressure above a threshold value that varies with material thickness. Below this threshold, the oxygen reaction with the steel surface is insufficient to fully clear the kerf, and dross forms. Laser cutting sheet metal services operators who know the correct pressure settings for each material and thickness produce consistently dross-free cuts. Those who run at default parameters may produce parts with dross that requires manual removal—a significant labor cost that erases the efficiency advantage of the laser cutting sheet metal services process.
Material Compatibility in Laser Cutting Sheet Metal Services
Laser cutting sheet metal services handle a broader range of materials than any other single thermal cutting method. Carbon steel, stainless steel, aluminum, brass, copper, titanium, and tool steel are all routinely cut on industrial laser cutting sheet metal services equipment. Each material has specific cutting parameter requirements—laser power, cutting speed, assist gas type and pressure—that the laser cutting sheet metal services operator must select correctly to produce quality cuts. The most common parameter error in laser cutting sheet metal services is running aluminum at cutting speeds optimized for steel, producing a rough edge with excess dross because the higher thermal conductivity of aluminum requires significantly slower cutting speeds to achieve the same energy input per unit time.
Thickness Ranges Handled by Laser Cutting Sheet Metal Services
Industrial laser cutting sheet metal services on 6-kilowatt fiber laser machines reliably cut carbon steel to 1.0 inch, stainless steel to 0.750 inch, and aluminum to 0.500 inch. Higher-power 12 to 15-kilowatt laser cutting sheet metal services extend these ranges to 1.250 inch carbon steel, 1.0 inch stainless, and 0.750 inch aluminum. Above these thickness ranges, the laser cutting process becomes increasingly marginal—requiring dramatically slower cutting speeds and producing rougher edges with larger heat-affected zones—and plasma or waterjet cutting services become more economical choices. Laser cutting sheet metal services shops typically publish their practical thickness capability as the range within which they can consistently produce dross-free, square-edged cuts without excessive parameter manipulation.
Selecting a Laser Cutting Sheet Metal Services Provider
The machine specification—the kilowatt rating, positioning accuracy, and maximum cutting envelope—is only the starting point for qualifying laser cutting sheet metal services providers. Ask the laser cutting sheet metal services supplier for a sample cut of your material and thickness, and inspect the edge quality with a 10x loupe or under a microscope. A reputable laser cutting sheet metal services provider will cut and ship a sample without hesitation because they are confident in their process. Ask about their cutting parameter database—whether they have proven parameters for your specific material grade and thickness, or whether they plan to extrapolate from similar materials. And ask about their kerf width tolerance: a laser cutting sheet metal services shop that knows its kerf width variation will provide a more accurate nested drawing quote than one that estimates material utilization from a generic nesting efficiency percentage.
Conclusion
Laser cutting sheet metal services deliver accuracy, edge quality, and speed that make them the preferred cutting method for most industrial fabrication applications. The accuracy advantages of laser cutting sheet metal services—±0.003 to ±0.005 inches positional accuracy, square edges on thin materials, minimal heat-affected zone, and narrow kerf widths—are real when the provider maintains their equipment, uses correct cutting parameters for each material, and replaces consumables on a defined schedule. Buyers who evaluate laser cutting sheet metal services providers on actual sample edge quality and documented cutting parameter experience—not just machine kilowatts and price—consistently find partners who deliver on the accuracy promises that laser cutting sheet metal services technology makes possible.
Frequently Asked Questions
What accuracy does laser cutting sheet metal services achieve?
Laser cutting sheet metal services on modern equipment achieves positional accuracy of ±0.003 to ±0.005 inches with repeatability of ±0.001 inches, supporting feature-to-feature tolerances of ±0.005 to ±0.010 inches on most part geometries.
What thickness can laser cutting sheet metal services handle?
A 6-kilowatt laser cutting sheet metal services machine reliably cuts carbon steel to 1.0 inch, stainless to 0.750 inch, and aluminum to 0.500 inch. 12 to 15-kilowatt machines extend these ranges to 1.250 inch, 1.0 inch, and 0.750 inch respectively.
Does laser cutting produce dross on the cut edge?
Properly set up laser cutting sheet metal services produces dross-free edges on carbon steel and stainless below the published thickness capability of the machine. Dross on a laser cutting sheet metal services edge indicates incorrect assist gas pressure or cutting speed settings.
What materials can laser cutting sheet metal services cut?
Laser cutting sheet metal services cut carbon steel, stainless steel, aluminum, brass, copper, titanium, and tool steel. Each material requires specific cutting parameters—gas type, pressure, and cutting speed—optimized for that alloy and thickness.
References
1. ISO 9013:2017, "Geometrical Product Specifications (GPS) — Cutting — Temperature Zones," International Organization for Standardization, Geneva, 2017.
2. ASTM B839-04(2019), "Standard Test Method for Measuring Kerf and Method of Characterizing the Cut Edge Produced by a Fusion Jet," ASTM International, West Conshohocken, 2019.
3. Powell, J., "CO2 Laser Cutting," 2nd Edition, Springer, London, 1998.
4. Steen, W.M. and Mazumder, J., "Laser Material Processing," 4th Edition, Springer, London, 2010.
5. Kalpakjian, S. and Schmid, S.R., "Manufacturing Engineering and Technology," 7th Edition, Pearson, Upper Saddle River, 2017.