
Every kilogram removed from a piece of equipment either increases its payload capacity, extends its battery range, or reduces its fuel consumption. For engineers designing equipment where weight matters—material handling platforms, portable power units, aerial work platforms, recreational vehicles—aluminum sheet metal fabrication is often the most practical path to the weight target without the cost and complexity of composite alternatives. But aluminum sheet metal fabrication is not the same process as carbon steel fabrication, and shops that apply steel fabrication thinking to aluminum often produce parts with dimensional problems, weld cracking, or surface finish defects. This article explains what actually matters in aluminum sheet metal fabrication for equipment builders.
Alloy Selection for Aluminum Sheet Metal Fabrication
The aluminum alloys used in aluminum sheet metal fabrication for equipment applications fall into two families based on their forming response and weldability. The 3xxx series (3003-H14, 3003-H16) provides moderate strength and excellent workability, making it the preferred choice for aluminum sheet metal fabrication of enclosures, ductwork, and non-structural covers where the part requires complex bending or drawing. The 5xxx series (5052-H32, 5052-H34) offers higher strength and better corrosion resistance, making it the standard for structural brackets, fuel tanks, and marine equipment fabricated by aluminum sheet metal fabrication. The 6xxx series (6061-T6) is the highest-strength option commonly available in sheet form, but its forming response is more limited than the 3xxx and 5xxx grades, making 6061-T6 better suited to aluminum sheet metal fabrication parts with simpler geometries that benefit from its yield strength of 40 ksi.
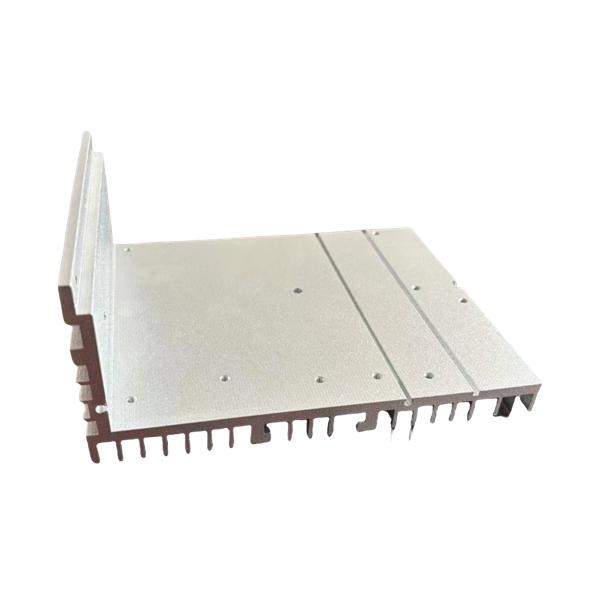
Temper and Formability in Aluminum Sheet Metal Fabrication
The temper designation—the -H or -T number that follows the alloy grade—describes the work-hardening or heat treatment state of the aluminum and directly determines its forming behavior in aluminum sheet metal fabrication. H32 temper aluminum is stabilized at a quarter-hard condition, providing a balance of formability and strength that is ideal for aluminum sheet metal fabrication parts requiring moderate bending. H34 (half-hard) is less formable but stronger, suitable for aluminum sheet metal fabrication parts with simpler bends where the higher strength is beneficial. The -T6 temper of 6061 aluminum provides the highest strength but is the most difficult to form without cracking, and any aluminum sheet metal fabrication involving 6061-T6 sheet should be reviewed for bend radius adequacy before quoting.
CNC Bending in Aluminum Sheet Metal Fabrication
Aluminum bends differently than steel, and aluminum sheet metal fabrication shops that understand this produce better parts at lower cost. The primary difference is springback: aluminum exhibits more springback than steel for the same bend angle because its modulus of elasticity is roughly one-third that of steel—68.9 GPa versus 200 GPa. A 90-degree bend in 0.125-inch 5052-H32 aluminum may spring back 3 to 5 degrees after punch release, compared to 1 to 2 degrees for the same bend in mild steel. The aluminum sheet metal fabrication operator must overbend accordingly, and the overbend amount must be empirically determined for each alloy-thickness-die combination because springback varies with material lot.
Tooling Selection for Aluminum Sheet Metal Fabrication Bending
The press brake tooling used for aluminum sheet metal fabrication should be dedicated or thoroughly cleaned between steel and aluminum work. Steel tooling with surface contamination—oil, chips, or oxidation from previous steel bending—can imprint into the relatively soft aluminum surface, creating scratches and die marks that are visible in the finished aluminum sheet metal fabrication part. Some aluminum sheet metal fabrication shops use polished or chromium-plated tooling specifically for aluminum to minimize surface marking. Additionally, the die opening width for aluminum sheet metal fabrication should be sized to the material thickness using an 8-to-1 die-width-to-thickness ratio rather than the 6-to-1 ratio commonly used for steel, reducing the required bending force and minimizing the risk of surface marking from excessive die pressure.
Welding Aluminum Sheet Metal Fabrication Components
TIG (GTAW) welding is the standard joining method for aluminum sheet metal fabrication because it produces the cleanest weld bead with the least spatter and the best cosmetic appearance on the relatively thin gauges common in equipment fabrication. MIG (GMAW) welding is also used in aluminum sheet metal fabrication for thicker sections above 0.125 inch, where the higher deposition rate of MIG reduces welding time. The filler alloy selection for aluminum sheet metal fabrication welding follows the base alloy: 4043 filler for welding 3xxx and 6xxx series aluminum, 5356 filler for welding 5xxx series aluminum. Using the wrong filler alloy produces welds with reduced strength or increased crack sensitivity in the aluminum sheet metal fabrication joint.
Weld Prep and Fit-Up in Aluminum Sheet Metal Fabrication
Cleanliness is the single most important variable in aluminum sheet metal fabrication welding. Aluminum has a tenacious aluminum oxide layer (Al2O3) with a melting point of 3,700°F—far above the 1,200°F melting point of the base aluminum beneath it. This oxide layer must be removed with a stainless steel wire brush dedicated to aluminum before welding, or the weld will be rejected for porosity and lack of fusion. Acetone or MEK wipe-down of the weld joint area removes machining oils and shop soil before welding. A reputable aluminum sheet metal fabrication shop maintains separate aluminum tooling, stores filler alloy in sealed containers to prevent moisture absorption, and performs weld sample testing to verify procedure adequacy before production welding.
Surface Finishing for Aluminum Sheet Metal Fabrication Parts
The surface finish options for aluminum sheet metal fabrication parts serve two purposes: corrosion protection and appearance. For most aluminum sheet metal fabrication parts in outdoor or humid environments, powder coating provides the best combination of durability and appearance. The aluminum surface is first chemically cleaned and etched, then a chromate conversion coating is applied to improve paint adhesion and provide sacrificial corrosion protection. The powder coat is then applied electrostatically and cured, producing a finish that withstands 1,000+ hours of salt spray exposure per ASTM B117 for aluminum sheet metal fabrication parts in demanding environments.
Anodizing as a Surface Finish for Aluminum Sheet Metal Fabrication
Type II anodizing produces a controlled aluminum oxide layer 0.0003 to 0.001 inch thick on aluminum sheet metal fabrication parts, improving corrosion resistance and providing a base for dye coloring. Type III hard anodizing produces a thicker oxide layer (0.001 to 0.003 inch) with surface hardness approaching 60 to 65 HRC, suitable for wear-critical aluminum sheet metal fabrication components. Anodizing requires that the aluminum sheet metal fabrication shop either has in-house anodizing capability or works with a qualified finishing partner. All anodized aluminum sheet metal fabrication parts must be masked at any tapped holes or critical bearing surfaces before anodizing, because the process builds up coating thickness on all exposed surfaces including internal threads.
Conclusion
Aluminum sheet metal fabrication for lightweight equipment is a specialized discipline that requires correct alloy selection, springback compensation specific to aluminum's lower modulus, dedicated aluminum tooling, and clean welding procedures. The shops that do it well treat aluminum as a different material family from steel—not just a lighter substitute—and adjust their forming parameters, welding procedures, and surface finishing accordingly. Buyers sourcing aluminum sheet metal fabrication parts should verify that their supplier has documented experience with the specific alloy and thickness being quoted, separate aluminum tooling or verified cleaning procedures, and a TIG welding process with documented filler alloy selection for the alloy being joined.
Frequently Asked Questions
What aluminum alloy is best for sheet metal fabrication structural brackets?
5052-H32 is the most commonly used alloy for structural aluminum sheet metal fabrication brackets due to its combination of yield strength (28 ksi), good formability, and excellent corrosion resistance in marine and outdoor environments.
How does springback differ in aluminum sheet metal fabrication compared to steel?
Aluminum sheet metal fabrication produces 2 to 3 times more springback than steel bending for equivalent geometries because aluminum's modulus of elasticity is approximately one-third that of steel, requiring significantly larger overbend angles to achieve target bend angles.
What welding method is used for aluminum sheet metal fabrication?
TIG (GTAW) welding is the standard for aluminum sheet metal fabrication on material below 0.125 inch, producing clean weld beads with minimal spatter. MIG (GMAW) is used for thicker aluminum sheet metal fabrication sections where higher deposition rate reduces welding time.
Can aluminum sheet metal fabrication parts be powder coated?
Yes. Aluminum sheet metal fabrication parts are cleaned, etched, and given a chromate conversion coating before powder coating, achieving 1,000+ hours salt spray resistance and excellent color durability in outdoor applications.
References
1. ASM Handbook Volume 2: "Properties and Selection: Nonferrous Alloys and Special-Purpose Materials," ASM International, Materials Park, 1990.
2. AWS D1.2/D1.2M:2014, "Structural Welding Code—Aluminum," American Welding Society, Miami, 2014.
3. ASTM B209-2014, "Standard Specification for Aluminum and Aluminum-Alloy Sheet and Plate," ASTM International, West Conshohocken, 2014.
4. Kalpakjian, S. and Schmid, S.R., "Manufacturing Engineering and Technology," 7th Edition, Pearson, Upper Saddle River, 2017.
5. Lancaster, J.F., "Metallurgy of Welding," 6th Edition, Woodhead Publishing, Cambridge, 1999.